Rectivas Materials
ISO 9001 quality management system held by the partner factory, covering formulation through packaging.
Flame retardant masterbatch is compounded and pelletized to our specification at our partner factory in Hebei — carrier resin matched to your process, dispersion checked before we ship a sample. Because we are not tied to one plant, the carrier and system are matched to your process rather than to one factory’s standard range. This page covers how we build a masterbatch grade and what to send us to get one started.
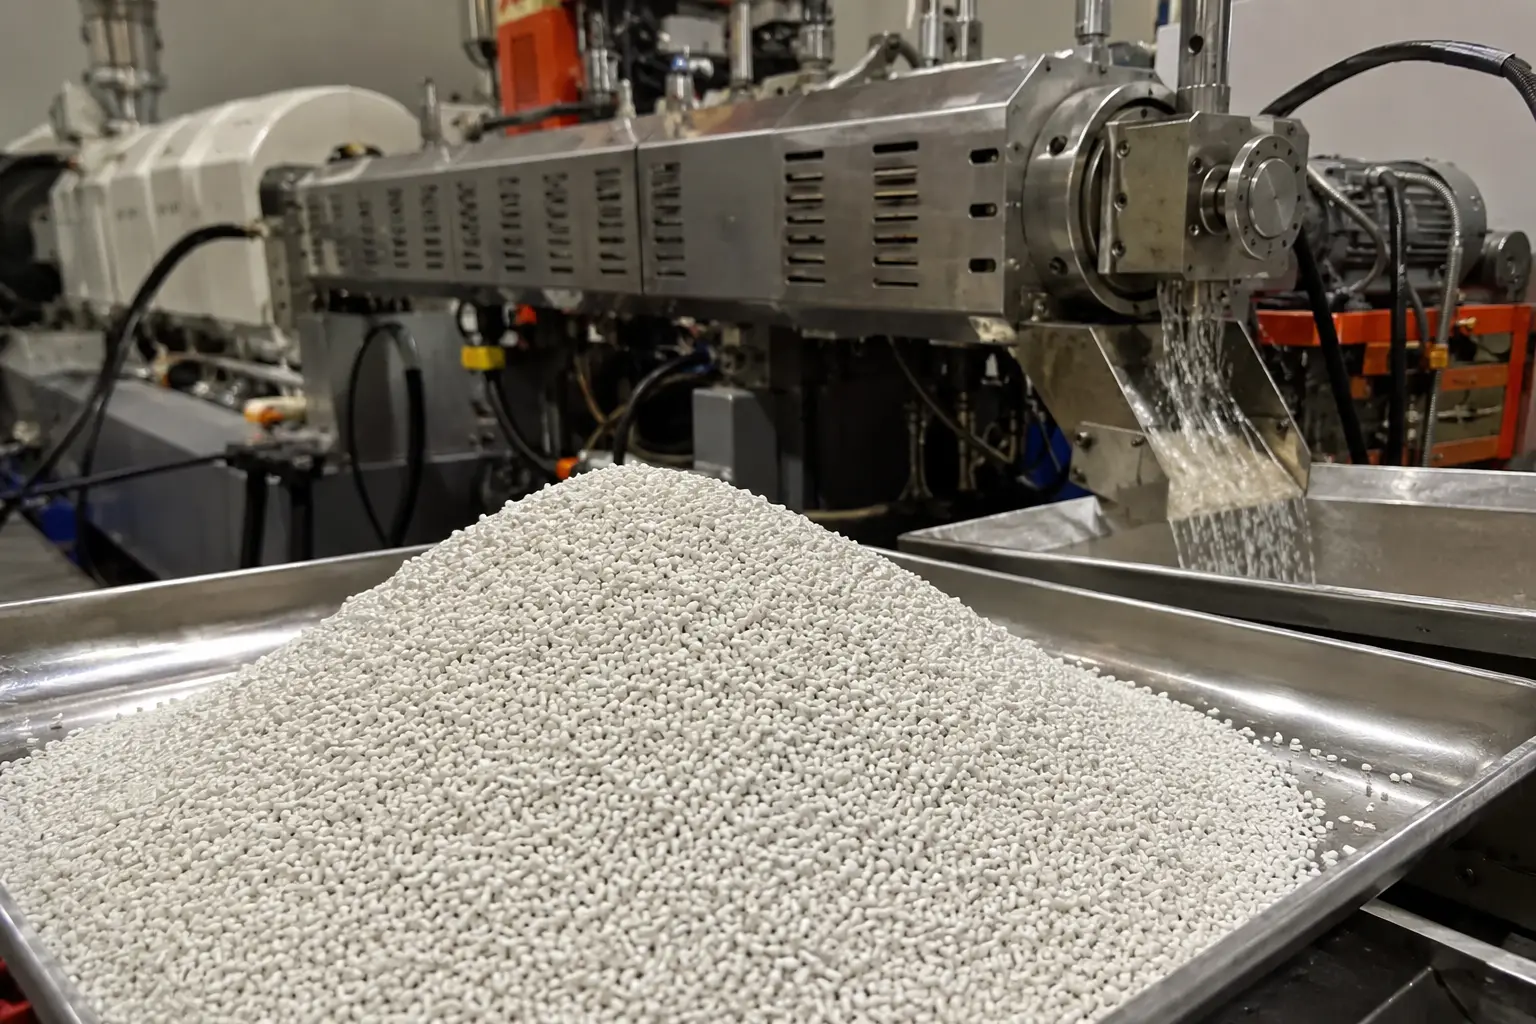 Fig. MB01 — masterbatch pellets, our partner factory’s production floor
Pellets compounded and pelletized to our specification at our partner factory.
Masterbatch pellets are made the same way our powder additives are — formulated, compounded on our partner factory’s SHJ-75 twin-screw extruder, pelletized, then burn-verified before a sample goes out.
ISO 9001 quality management system held by the partner factory, covering formulation through packaging.
Twin-screw compounding followed by pelletizing at the partner factory — the same equipment behind every carrier grade we quote.
Let-down trials and UL94 burn testing arranged at our partner factory before a masterbatch grade is recommended.
| Carrier | System | Typical Use |
|---|---|---|
| PP carrier | Halogen-free / brominated | Injection molding, extrusion let-down into PP |
| PE carrier | Mineral / halogen-free | Film, pipe, cable, molding into PE/HDPE/LDPE |
| PVC carrier | Antimony / zinc borate systems | Cable, profile, sheet PVC compounds |
| EVA / custom carrier | Project-dependent | Cable jacket and specialty let-down applications |
Resin, melt index and process matched so let-down is clean at your line speed.
Bags and big bags discussed to your specification for bulk orders.
Every new carrier grade starts with a sample for your own dosing trial.
Trial and repeat volumes confirmed per project — tell us your target.
Appearance, moisture and let-down consistency checked before dispatch.
Standard document set issued per shipment.
Third-party test reports on RoHS/REACH-regulated substances available per product.
Held by the partner factory, covering formulation through shipment.
Resin, let-down ratio and processing method.
Carrier and system matched to your line.
Sample shipped, dosed and burn-verified.
Packaging, documents and shipping confirmed.
Masterbatch is the easiest flame retardant format to mis-buy, because two quotes can look 20% apart on price and be identical in real cost — or the reverse. Three things decide it, and none of them is the number on the quotation.
| Ask Every Supplier | Why It Changes the Real Price |
|---|---|
| “What is the active content?” | The single most important question. A masterbatch at 40% active against one at 60% is not 20% cheaper — you will dose half as much again to hit the same loading. Normalise every quote to price per kilo of active before you rank them. |
| “Which carrier resin, and what MFI?” | At a 30% let-down ratio the carrier is roughly a third of what you are buying, and it stays in your part. A mismatched carrier quietly changes impact and flow you had already qualified. |
| “Was the sample line-produced?” | Lab-made samples disperse better than production lots. Ask for the lot number and whether the same twin-screw line will run your order. |
| “What is your batch-to-batch tolerance on active content?” | A supplier who cannot answer this in numbers is not measuring it. Drifting active content shows up as a UL94 result that passes in spring and fails in autumn. |
Our position on each, plainly. We state active content on the TDS and hold it under ISO 9001 batch control, samples come off the same SHJ-75 line that runs production orders, and carrier resin is specified rather than left as “universal” — because a universal carrier is a compromise someone else made for you. Ask for trial quantity and production MOQ in the same enquiry so you can plan qualification properly. And if you are running high loadings, ask whether finished compound is cheaper for you than dosing masterbatch at all; above roughly 40–50% it usually is, and we would rather tell you that than sell you the harder route.
Neither label fits cleanly. Rectivas is a sourcing and technical partner: masterbatch is compounded and pelletized to our specification on a partner factory’s twin-screw line in Hebei, and every lot is traceable to the line that produced it.
Yes — carrier resin is matched to your process (PP, PE, EVA, PA or a project-specific carrier) so the masterbatch disperses cleanly at your let-down ratio.
Order volumes are confirmed per project rather than fixed to one number — tell us your trial or repeat-order target and we will confirm what is workable for your carrier and system.
Yes — send your carrier resin, target let-down ratio and flame rating, and we will propose a masterbatch grade and arrange a sample for your own dosing trial.
Yes — repeat-order volumes for resale are supported, with the same batch-to-batch consistency and document set as a direct end-user order.
Send your carrier resin, target let-down ratio, flame rating and order volume. We’ll confirm the grade, the sample process, and what’s realistic for your project.